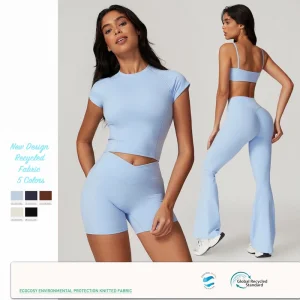
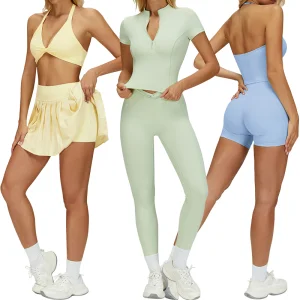
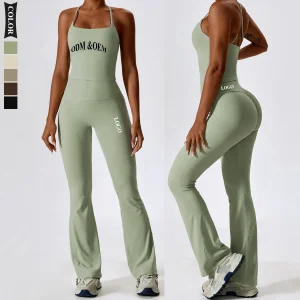
The global sportswear industry is undergoing a seismic shift. No longer is "performance" the only metric for success; sustainability has become the new benchmark. As of 2024, the recycled sportswear market is projected to grow at a CAGR of over 12%, driven by increasing environmental awareness among Gen Z and Millennial consumers. From high-street fashion brands to specialized athletic labels, the demand for apparel made from rPET (recycled Polyethylene Terephthalate) and Recycled Nylon (Econyl) is skyrocketing.
Major economies in North America and the European Union have introduced stringent regulations regarding textile waste and carbon footprints. This has forced global procurement officers to look for a Top Best Recycled Sportswear Factory that not only offers competitive pricing but also holds international certifications like GRS (Global Recycled Standard), OEKO-TEX, and BSCI. The commercial reality is simple: brands that fail to integrate recycled materials into their supply chain face both regulatory penalties and consumer boycotts.
The industry is moving beyond simple recycling. We are now seeing the integration of AI-driven design to minimize fabric wastage during the cutting process. As a leading supplier, we utilize automated 3D garment rendering to reduce the need for physical samples, further lowering our carbon footprint. Smart fabrics that offer both compression and breathability while being 100% sourced from post-consumer waste are becoming the gold standard.
Moreover, circularity—the concept of a garment being fully recyclable at the end of its life—is the ultimate goal. This involves using mono-materials that can be chemically broken down and repurposed without losing structural integrity.
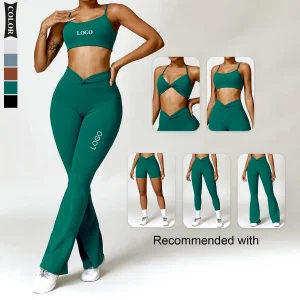
Today's B2B buyers—from boutique yoga studios in Los Angeles to fitness franchises in Berlin—are no longer just looking for a "vendor." They are looking for a strategic manufacturing partner. The primary procurement needs in the recycled sportswear sector include:
Recycled sportswear has transitioned from a niche "organic" product to a mainstream performance essential. In North America, there is a massive surge in "Athleisure" where recycled yoga sets are worn from the office to the gym. In Europe, the focus is on high-performance running and cycling gear that meets strict environmental "Green Deal" criteria.
In the Asia-Pacific region, the rise of outdoor lifestyle activities like glamping and hiking has created a demand for durable, quick-dry, and moisture-wicking recycled apparel that can withstand various climates.
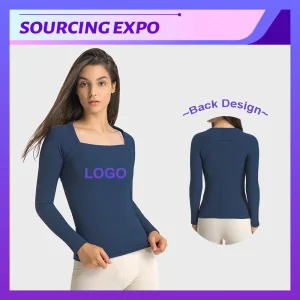
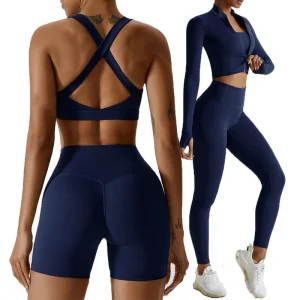
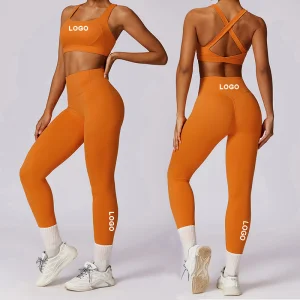
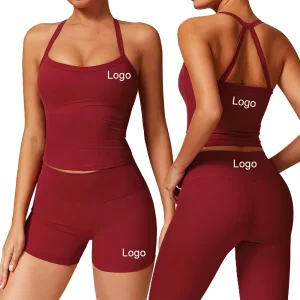
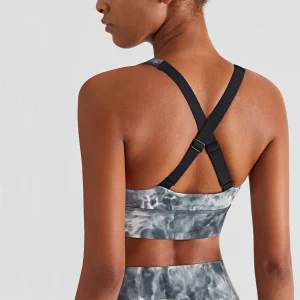
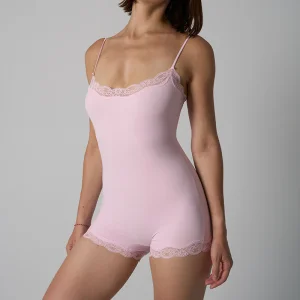
Guangzhou Reba Fashion Co., Ltd. is a professional manufacturer specializing in modern activewear and lifestyle apparel. Located in Guangzhou, China, the company focuses on the design, production, and export of high-quality sports and casual clothing for global markets. Our main product range includes yoga wear, fitness wear, gym wear, workout sets, sports bras, bodysuits, crop tops, tank tops, compression wear, running wear, training wear, activewear sets, lounge wear, stretch wear, performance wear, athleisure wear, dance wear, and cycling wear. These products are designed to provide comfort, flexibility, and style for sports, workouts, and everyday activities.
Founded in 2016, Guangzhou Reba Fashion Co., Ltd. began as a small garment workshop and gradually developed into a reliable supplier in the activewear industry. The company currently employs more than 110 skilled workers, including experienced designers, technicians, and quality control staff. Our modern production facility covers approximately 7,500 square meters and is equipped with advanced garment manufacturing and sewing equipment to ensure efficient production and consistent quality.
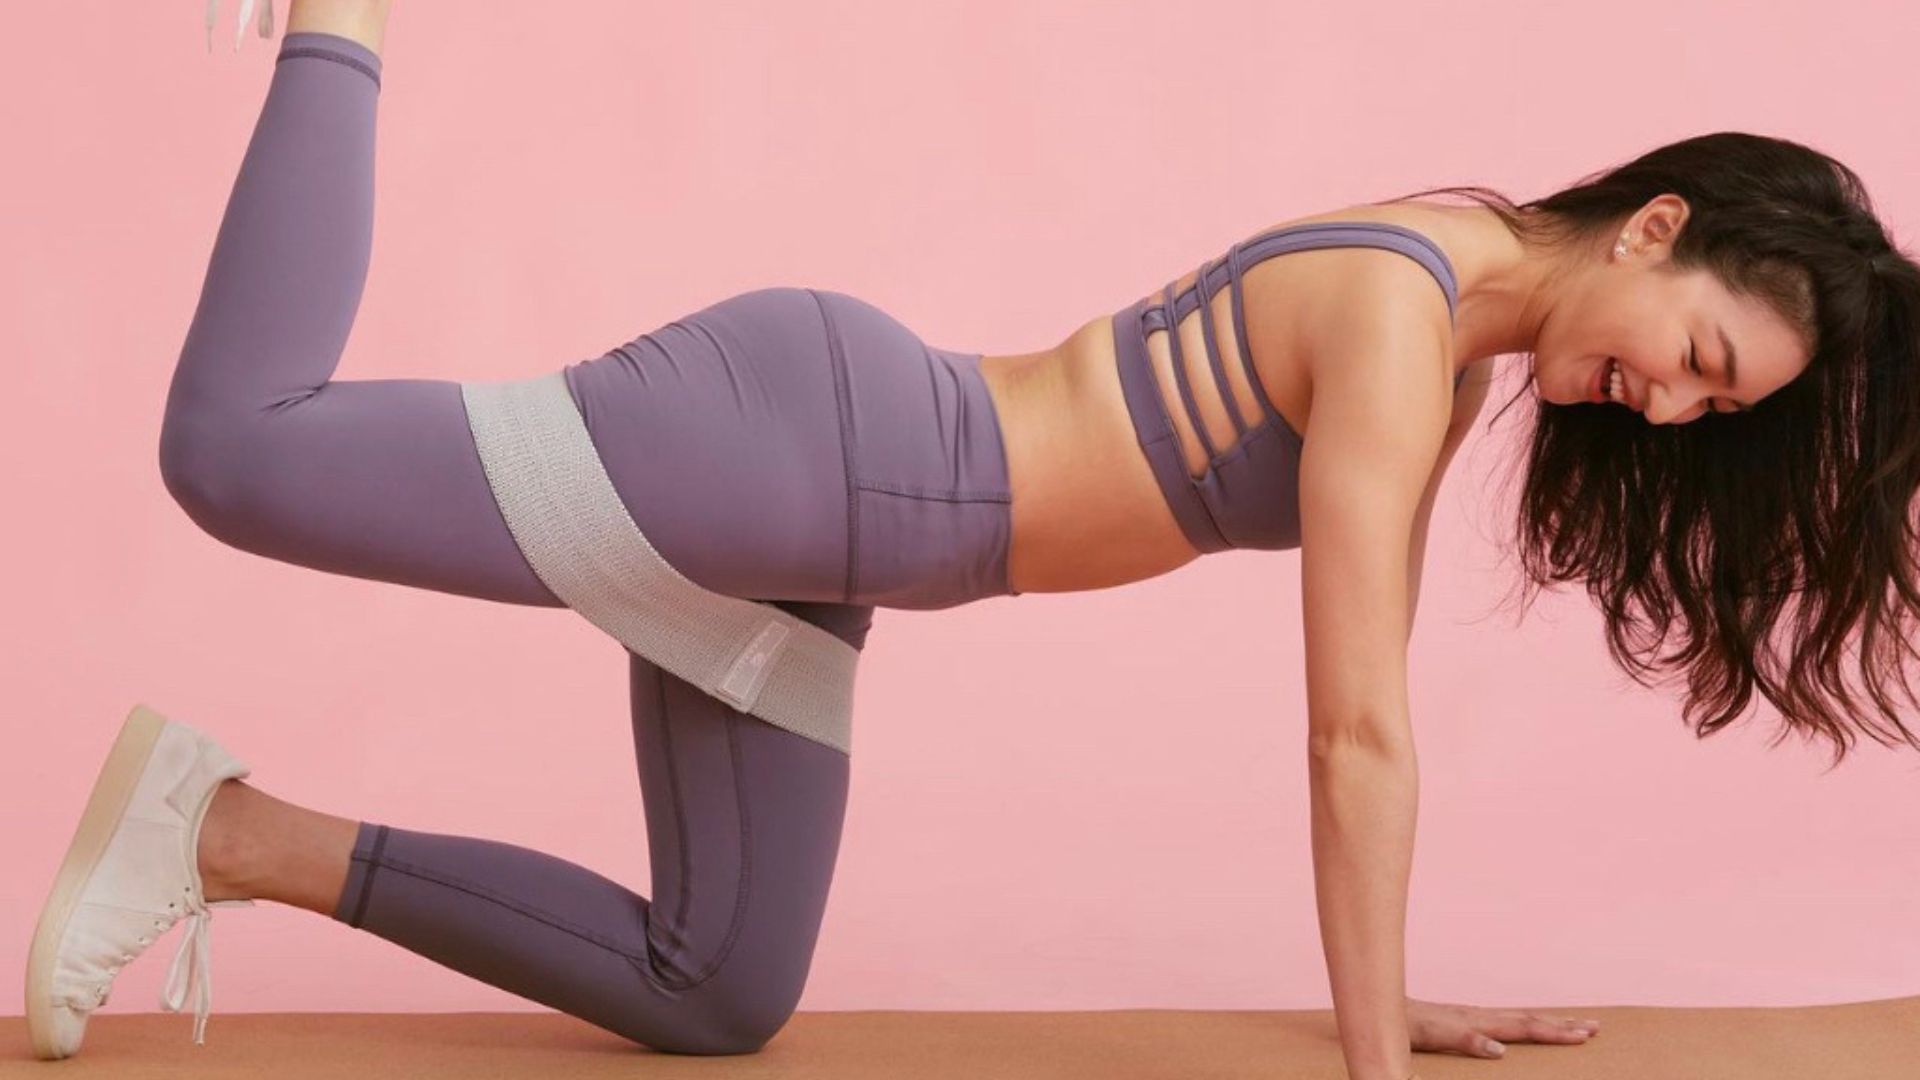
Operating out of Guangzhou—the global hub for textile innovation—gives us unparalleled advantages. We have direct access to the world's most advanced recycled fiber spinning mills. This proximity allows us to source the latest eco-fabrics before they even hit the international market. Our integration of the supply chain means we can offer factory-direct pricing without the middleman markup, all while adhering to the highest international labor and environmental standards.
Over the years, Reba Fashion has established long-term partnerships with clients in Europe, North America, Southeast Asia, and other international markets. With a strong commitment to innovation, quality control, and customer satisfaction, the company strives to deliver fashionable and functional activewear solutions to customers worldwide.
At Guangzhou Reba Fashion, we believe that the future of fashion is circular. Every piece of recycled sportswear that leaves our factory represents a commitment to reducing plastic waste in our oceans and landfills. We utilize low-impact dyes and water-recycling systems in our dyeing processes to ensure that our environmental responsibility extends beyond just the fabric we use.
Our quality control team performs rigorous testing on every batch, checking for color fastness, elasticity retention, and moisture-wicking efficiency. We understand that for a recycled product to be truly sustainable, it must be durable. A garment that lasts for years is far better for the planet than a "fast fashion" item that ends up in a landfill after three washes.
 Reba Fashion